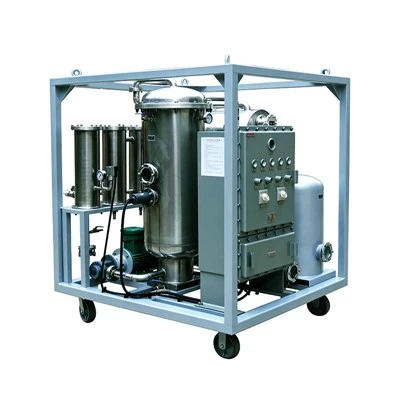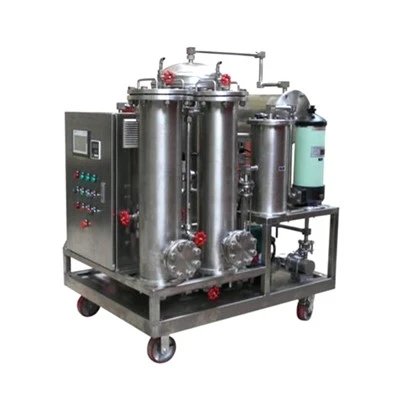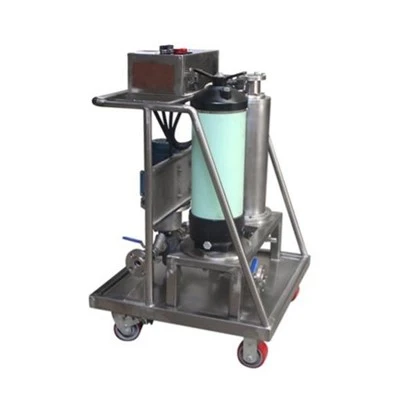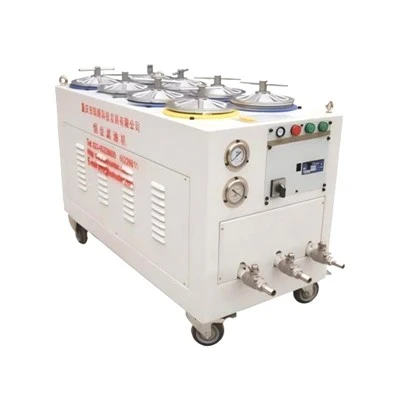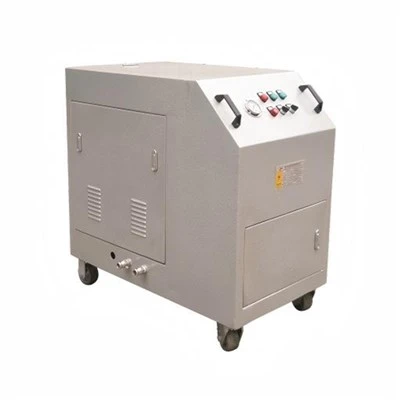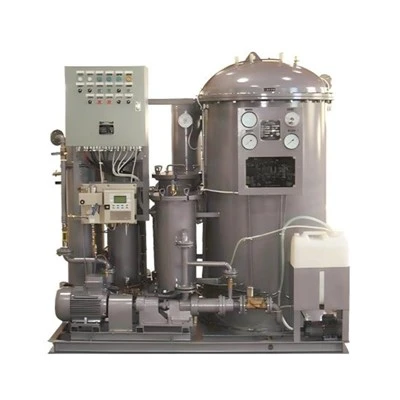

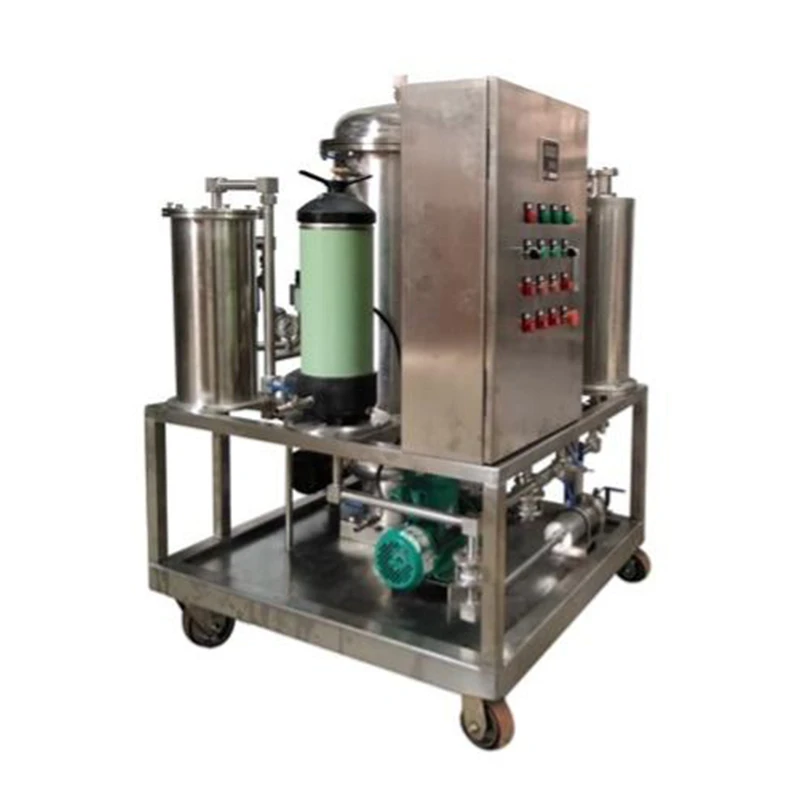
Chongqing Lushun Scientific & Technological Development Co., Ltd. is one of the leading manufacturers and suppliers of zt-i-z vacuum phosphate ester fire-resistant oil purifier in China. With abundant experience, we are committed to providing high quality customized products with competitive price. Please feel free to buy advanced zt-i-z vacuum phosphate ester fire-resistant oil purifier from our factory. Also, quotation is available.
ZT-I-Z Vacuum Phosphate Ester Fire-Resistant Oil Purifier
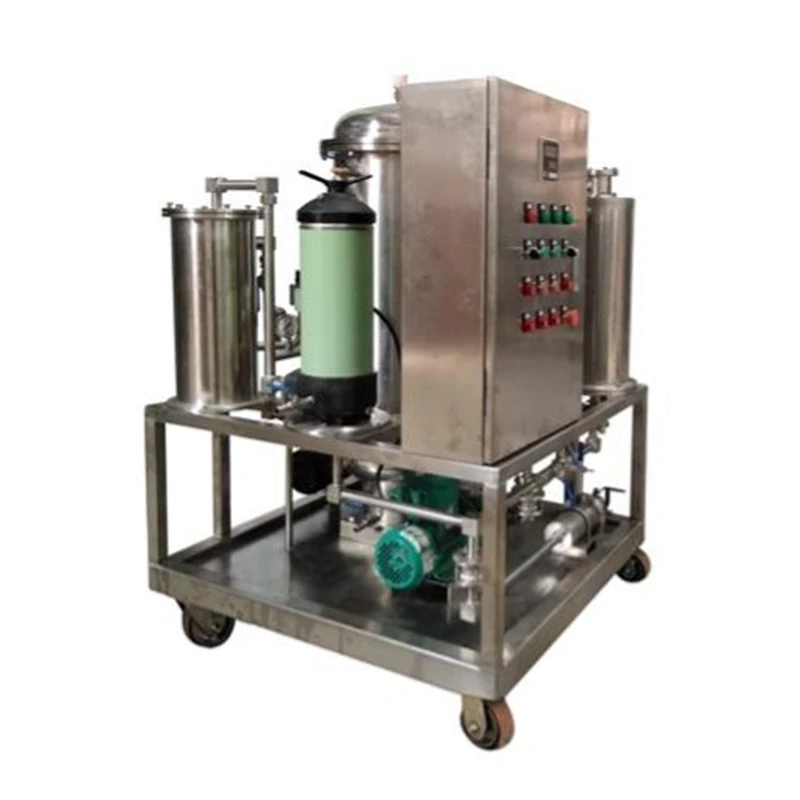
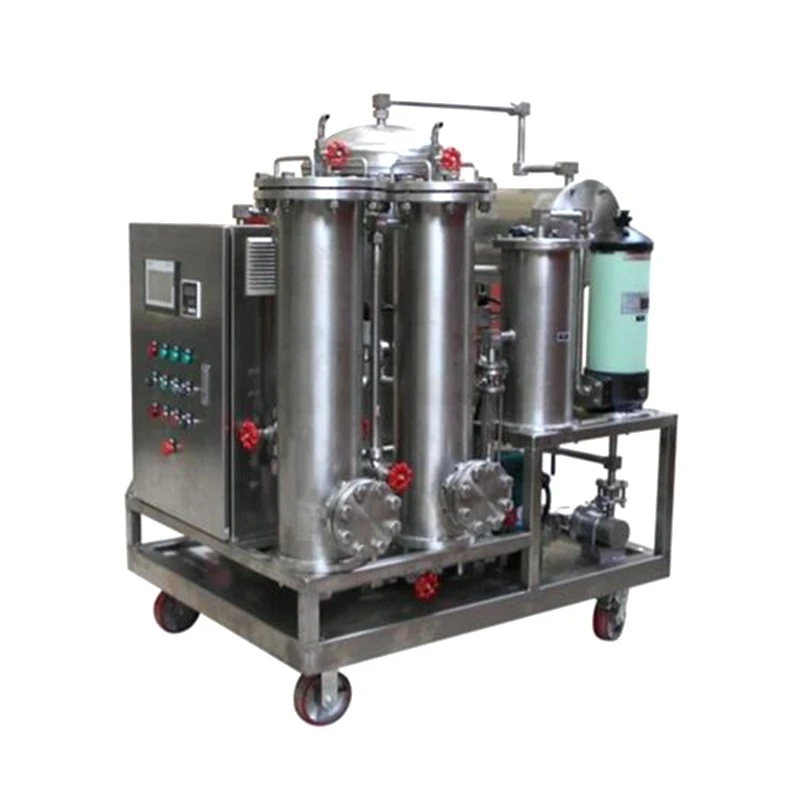
ZT-I-Z Series Vacuum Phosphate Fire Resistant Oil Purifiers are the dedicated equipment for phosphate fire resistant oil purification. Adopting stainless steel and fluororubber sealing materials, they are multifunctional regeneration and purification vacuum oil purifiers with functions of degassing, dehydration, and impurity removal. And they have also functions of topping up and pumping oil. Online moisture detector, particle detector and PLC intelligent controller can be matched as their optional components.
Technical Specification
|
Flow Rate |
20L/min |
|
Rated Pressure |
≤0.5Mpa |
|
Working Vacuum Degree |
-0.08~-0.098Mpa |
|
Power Supply |
380V/50Hz |
|
Heating Power |
10KW |
|
Total Power |
12KW |
|
Net Weight |
400Kg |
|
Overall Dimension (L×W×H) |
1200mmx1050mmx1600mm |
|
Particle Contamination (NAS1638) |
≤6 grade |
|
Water Content (mg/L) |
≤1000(GB/T7600) |
|
Inlet/Outlet Diameter |
20mm |
Advantages
Specifically designed for phosphate ester fire-resistant oil: The entire unit is made of stainless steel and fluoro rubber seals, ensuring excellent chemical stability and sealing reliability when handling highly corrosive oils, thereby extending the equipment's service life.
Efficient purification and regeneration capabilities: Equipped with strong polarity molecular adsorbents and dry ion exchange resins, it not only removes moisture, gases, and impurities but also effectively reduces the acid value and increases resistivity. This solves electrochemical corrosion issues and reduces the frequency of servo valve replacements.
Multi-functional integrated processing: It integrates functions such as degassing, dehydration, impurity removal, acid value reduction, resistivity improvement, oil color enhancement, and the removal of sludge and gels, comprehensively improving the overall performance of the oil.
High-precision filtration guarantee: Utilizing a 1-micron filter, it ensures that the particle contamination level of the treated oil is ≤ Grade 6 (NAS1638), meeting the strict cleanliness requirements of precision hydraulic systems.
Intelligent and expandable: It offers optional online moisture detectors, particle detectors, and a PLC intelligent control system, enabling automated monitoring and data recording to improve operation and maintenance efficiency.
Compact structure and easy operation: It features a three-dimensional vacuum flash evaporation system with a large oil-water evaporation area for high processing efficiency. It also supports high-altitude oil pumping and low-level oil suction, adapting to various on-site conditions with flexible installation.
Application
ZT-I-Z Series Vacuum Phosphate Fire Resistant Oil Purifier is a professional machine to purify phosphoric acid ester anti-fuel oil. This machine is multi-function vacuum oil purifier which is made of stainless steel and fluoro rubber seal material.
FAQ
Q: What core purification challenge does the ZT-I-Z Series machine address for phosphate-ester fire-resistant oil systems?
A: Apart from conventional removal of gas, water and solid contaminants, the unit targets chemical degradation of phosphate-ester fluid. It leverages molecular adsorption and dry ion-exchange to eliminate polar hydrolysis by-products, restore oil resistivity and mitigate electrochemical corrosion risk inherent to DEH servo valve assemblies, rather than only performing physical filtration.
Q: What practical operational benefits can be gained from adding optional online detectors and PLC control system?
A: Manual periodic sampling and laboratory testing introduces obvious time lag. The optional online moisture detector and particle counter coupled with PLC enable continuous real-time oil-quality trending. It supports threshold-based alarm, automatic start-stop of purification cycle and data logging, facilitating condition-based maintenance instead of fixed-schedule manual operation for power-plant hydraulic systems.
Q: How do flow rate and vacuum parameters affect actual purification performance on-site?
A: Rated flow 20 L/min defines the theoretical processing capacity; excessively high actual flow shortens fluid residence time inside vacuum chamber and weakens dehydration effect. Working vacuum range of -0.08 ~ -0.098 Mpa must be strictly maintained. Too-deep vacuum may trigger local thermal decomposition of phosphate-ester oil, while insufficient vacuum lowers degassing-dehydration efficiency.
Q: What constraints should be considered regarding footprint and weight during field layout planning?
A: Compact overall dimension and net weight reduce space occupation, yet users shall reserve sufficient clearance for filter element replacement, adsorbent media overhaul and heat dissipation ventilation. Avoid enclosed narrow cabins with poor air circulation; vibration isolation measures are recommended when installing on floating platforms or compact skid-mounted power modules.
Q: What value do built-in oil-pumping and low-level suction functions bring to system maintenance workflow?
A: These auxiliary functions are not intended for continuous bulk oil transfer. They serve the maintenance phase of fire-resistant oil systems: completing oil replenishment, partial oil draining and fluid switching without deploying separate transfer pump. Users need to avoid long-duration pure pumping operation, which may cause overload and accelerate internal component wear.
Hot Tags: zt-i-z vacuum phosphate ester fire-resistant oil purifier, China zt-i-z vacuum phosphate ester fire-resistant oil purifier manufacturers, suppliers, factory